Pharmaceutical Packaging
Pharmaceutical supply chains run on control. Every material, every surface and every supplier is documented, audited and accounted for. Then a timber pallet of unknown history rolls into the warehouse, and it’s the least controlled thing in the building.
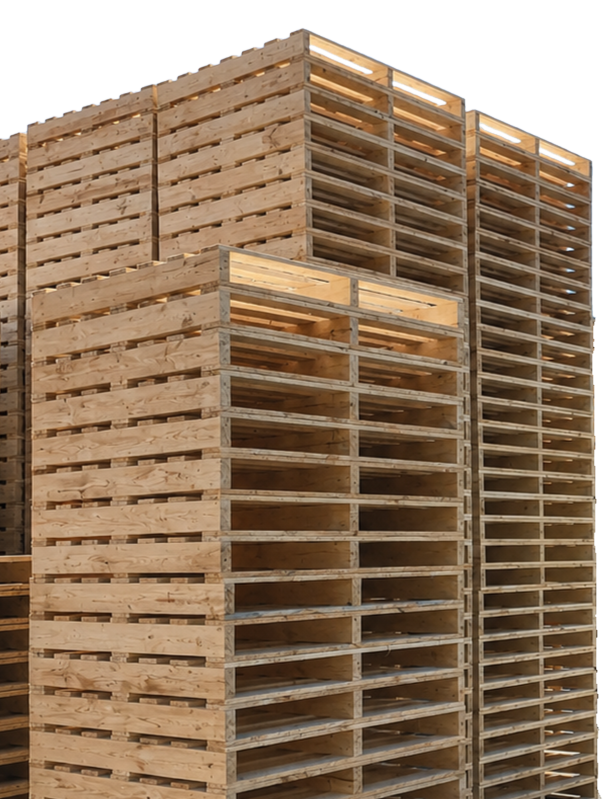
CMTP supplies the pharmaceutical industry with packaging that holds up to the same scrutiny as everything else in your operation: HACCP certified pallets, chemical-free heat-treated timber, and engineered crating for the equipment your production depends on. Made at the nearest of eleven Australian sites and delivered on schedule.
A pharmaceutical packaging supplier you can audit
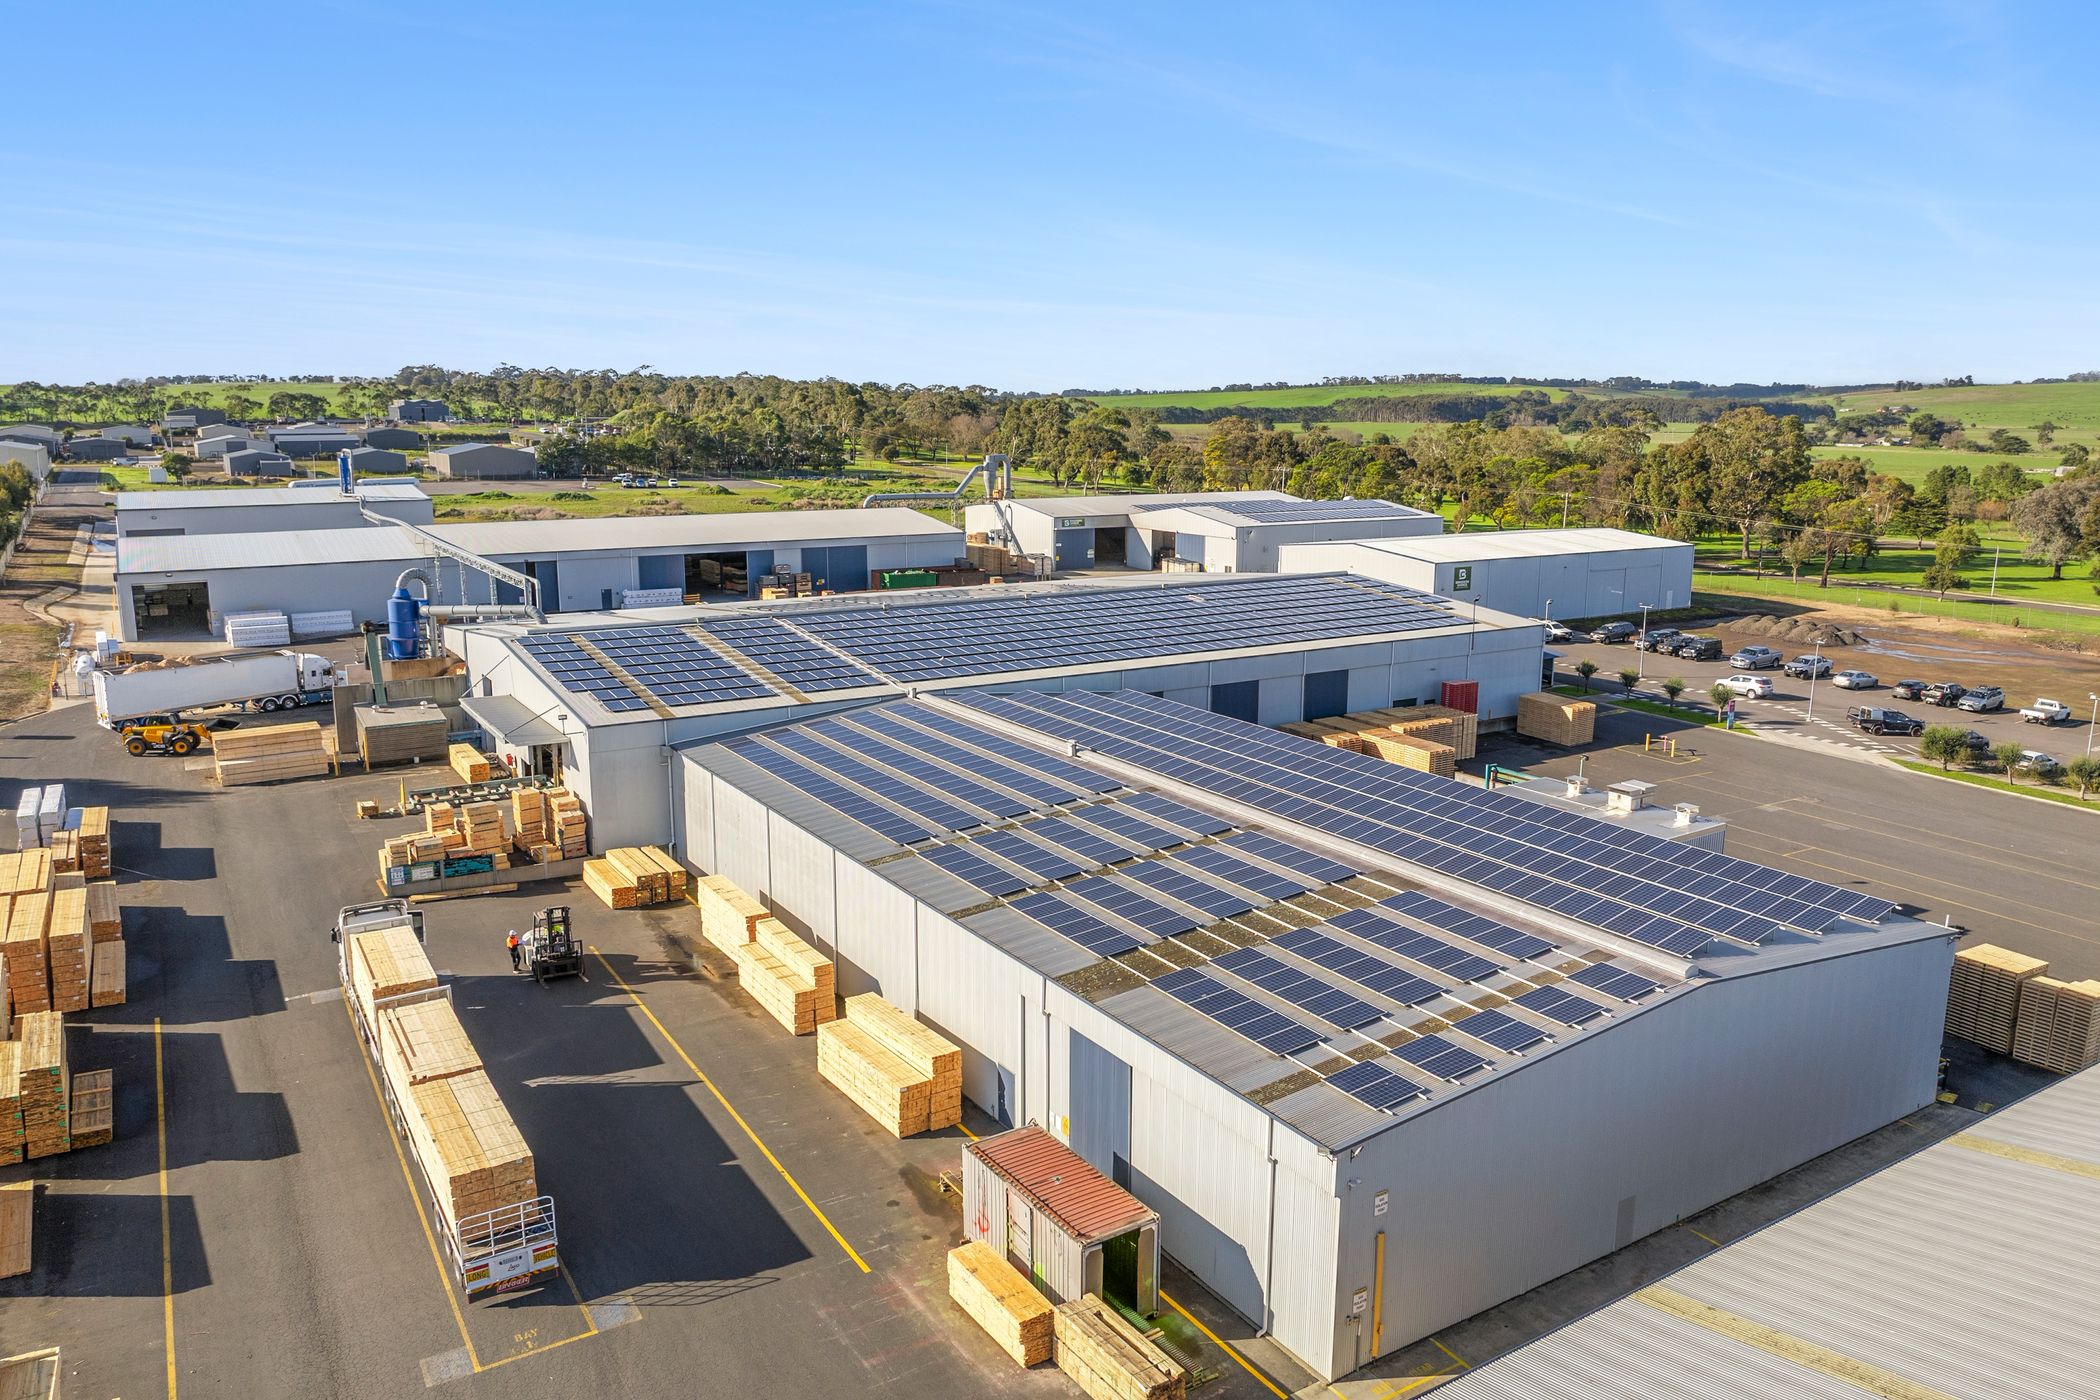
CMTP has been making packaging since 1976, when the business started in a workshop in Colac, Victoria. It is still family owned and still run by the family that started it. Around 250 people work across eleven manufacturing sites in Victoria, New South Wales, Queensland, South Australia and Tasmania.
In a GMP environment, who made a thing matters as much as what it is. We manufacture pharmaceutical pallets on our own equipment at our own sites, from timber we can trace, so the answers to an auditor’s questions come from us rather than from whoever we bought from. ISO 9001 quality management runs at Colac and Dandenong. CMTP is also the only timber pallet supplier in Australia holding HACCP International certification, and that certification covers pharmaceutical alongside food and beverage.
Hygienic pallets, plastic pallets for wash-down areas, chemical-free heat-treated timber and engineered crating for production equipment all come from the one place, which keeps pharmaceutical logistics down to one supplier and one specification across every site you run. Design and engineering sits in house, so medical packaging and GMP packaging is measured, designed and prototyped before a production run rather than adapted from a stock size. Pharma packaging carries a confirmed delivery date against a 95 per cent DIFOT target.
What goes wrong with pharmaceutical packaging
A standard pallet arrives with no history: where it’s been, what it carried, what it was treated with. In a GMP environment that’s not a pallet, it’s an uncontrolled input, and it becomes your problem the moment an auditor asks about it.
Damp timber brings moisture into climate-controlled storage, and moisture brings mould. In most industries that costs cartons. In pharmaceuticals it can cost the stock, the storage zone and a deviation report nobody wants to write.
Production and lab equipment is sensitive, calibrated and brutally expensive to replace. Moving it in, out or between facilities in packaging that wasn’t engineered for it puts the whole production schedule on the line, not just the machine.
How CMTP solves them
Through the Pal-giene manufacturing process, CMTP is the only HACCP International certified pallet supplier in Australia, and the certification explicitly covers pharmaceutical use. Every pallet arrives new, from a documented process, with an answer for the auditor. Plastic pallets cover zones that need washdown.
Our timber is heat treated (minimum 56 degrees for 30 minutes), not chemically fumigated, so there are no treatment chemicals near your product. Kiln-drying controls moisture content before the pallet ever enters your storage, keeping mould risk out of the building.
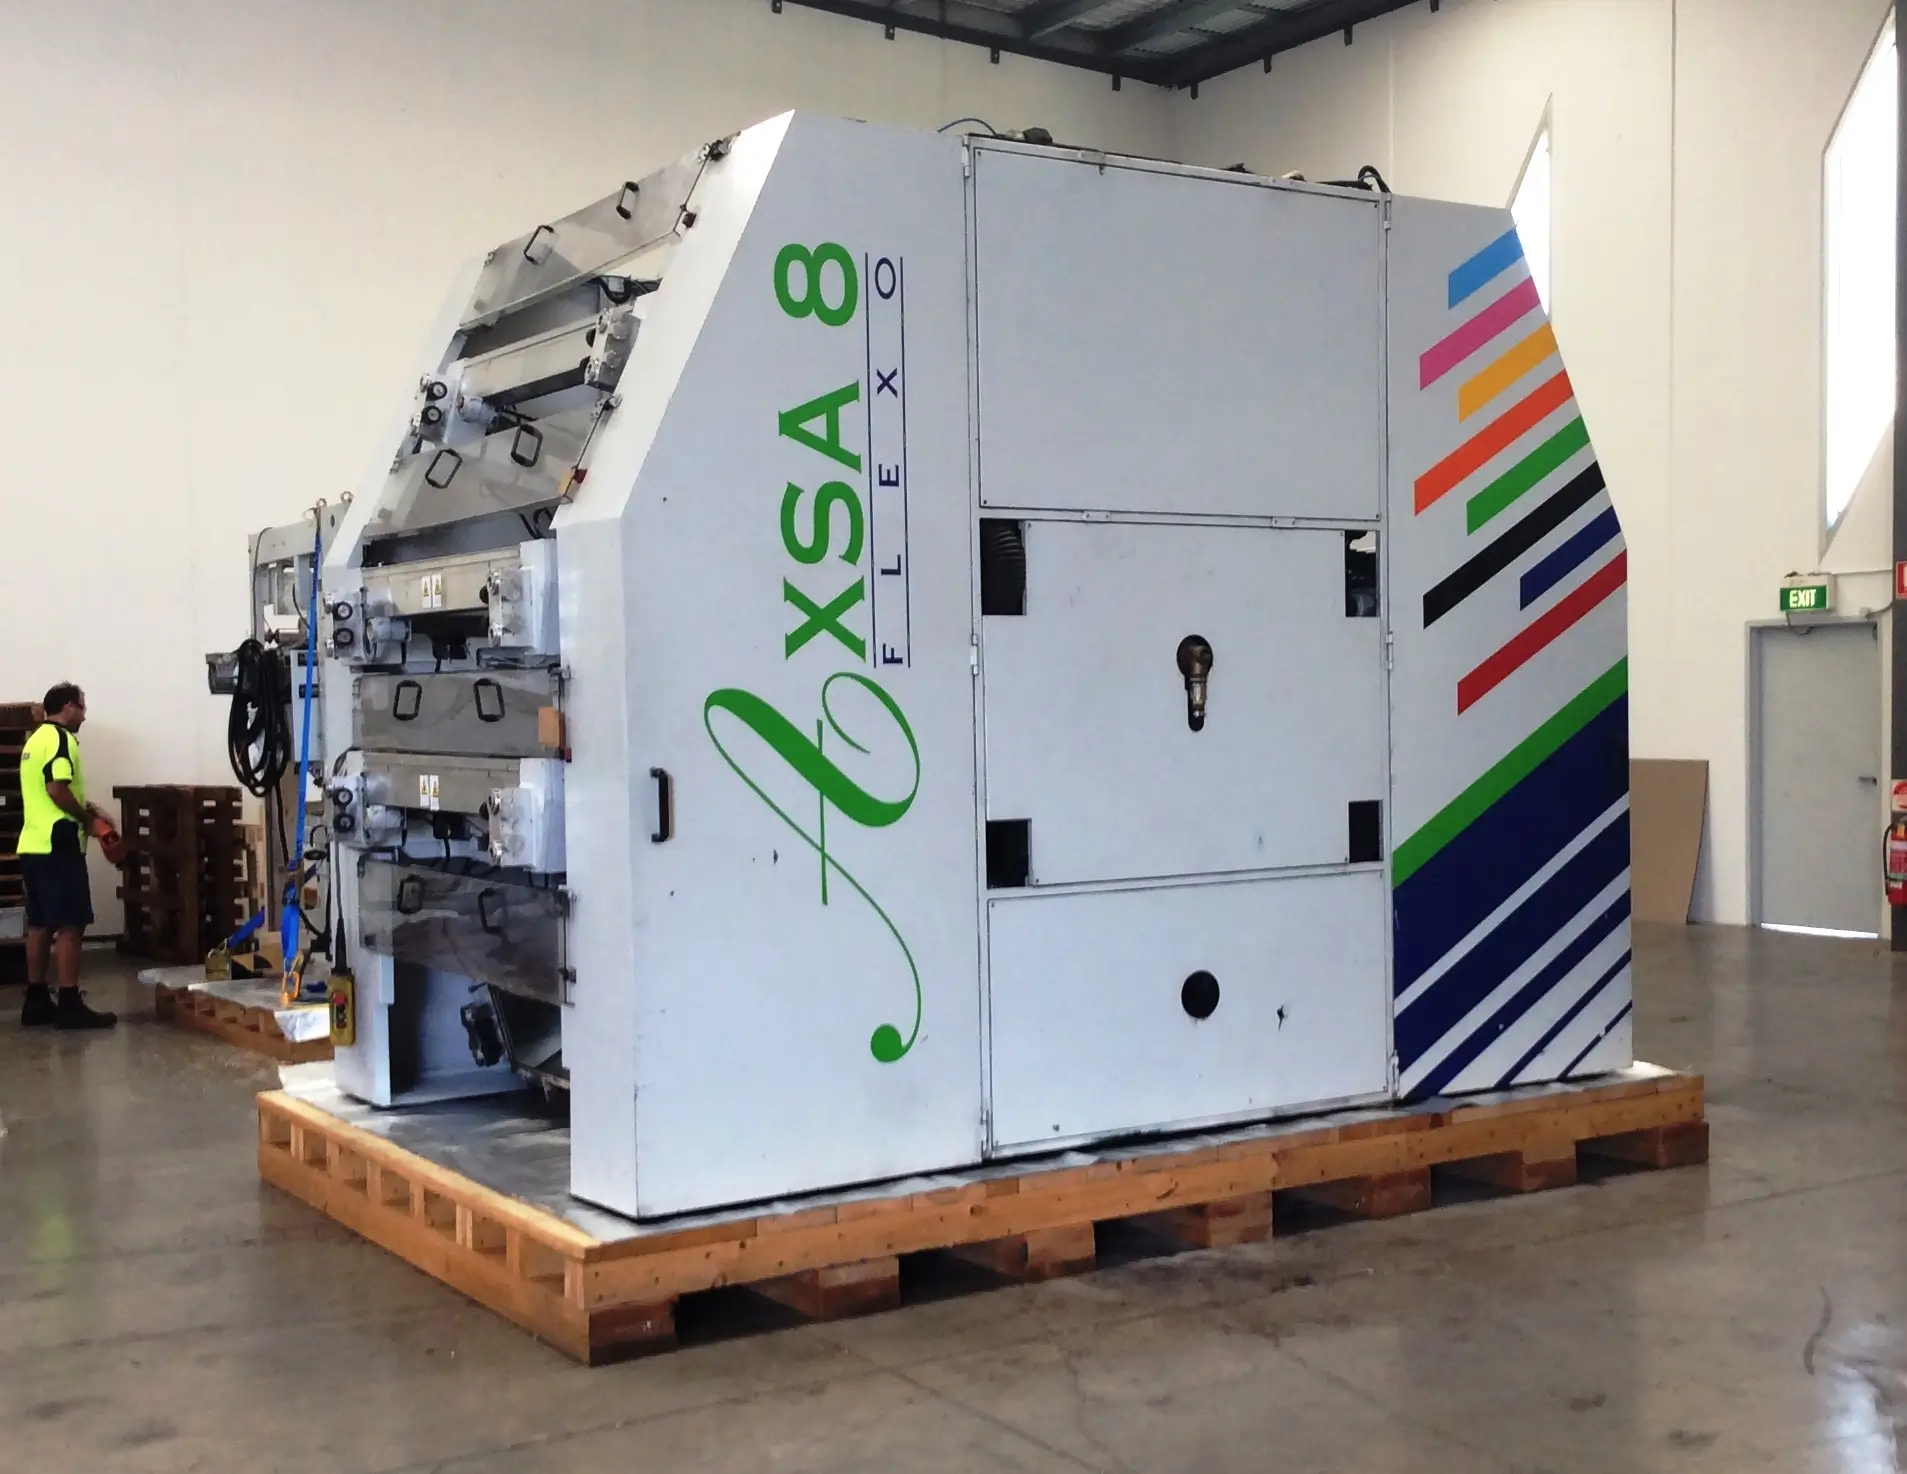
Our machinery packing teams measure equipment where it sits, design crating around it, and pack on site with inducted, OH&S compliant crews. Corrosion protection and short or long term storage are there when the install schedule moves.
Products built for pharmaceuticals
Each links to its product page:

HACCP certified pallets
HACCP International certified through the Pal-giene process, covering pharmaceutical use

Plastic pallets
hygienic, washable, for controlled and washdown zones

Packaging Built to Suit
stamped and compliant for pharmaceutical exports

Wooden cases and crates
engineered crates for equipment and high-value freight

Corrosion protection packaging
VCI and barrier systems for stored and shipped equipment
-
 ISO 9001 Certified - Colac
-
ISO 9001 Certified - Dandenong
-
 ISPM 15 Certified
-
 HACCP Certified
Get your obligation free quote
Related Services

Machinery Packing
engineered crating for production and lab equipment moves

Design & Engineering
packaging designed around the product and the compliance requirement, prototyped first

Logistics & Delivery
scheduled supply against a 95 per cent DIFOT target

Contract Packaging
inducted teams packing at your facility, under your site rules
Australia-wide Service
With teams across 11 manufacturing facilities across Australia, we’re able to reach your location quickly and provide the service you need on time.
Victoria
Colac – Head Office
Derrimut
Dandenong South
Mildura
New South Wales
Albury
Glendenning
Queensland
Clontarf
Brendale
South Australia
Adelaide
Tasmania
Branxholm
Scottsdale
Frequently Asked Questions
Do you supply HACCP certified pallets for pharmaceutical use?
Yes. CMTP’s Pal-giene manufacturing process is HACCP International certified, and we’re the only Australian pallet supplier to hold that certification. It covers pharmaceutical, food and beverage use, so you get a pallet with a documented, hygienic history instead of an unknown one. Ask the team about our foodXP pallets.
Are your pallets treated with chemicals?
No. Our timber is heat treated to a core temperature of at least 56°C for a minimum of 30 minutes, with no fumigants or chemical treatments anywhere near your product. It’s also kiln-dried to keep the moisture down, which stops mould forming in climate-controlled storage.
Will your pallets pass a GMP audit?
They’re built to. Every pallet is new, made from traceable timber and comes out of a HACCP International certified process with a documented history, which answers the questions a GMP auditor asks about incoming materials. If your site works to a stricter standard, the team will match the pallet to it, in timber or plastic for washdown areas.
Can you crate and move pharmaceutical production equipment?
Yes. Our machinery packing team measures your equipment where it sits, designs a crate around it and packs it in place, with crews inducted to work on your site. For moves or installs on a tight schedule, we can add corrosion protection and store the crated equipment until the receiving site is ready.
Can you supply export packaging for pharmaceutical shipments?
Yes. Our export pallets and crates are ISPM 15 compliant and individually stamped, so they clear biosecurity at the destination. Because ISPM 15 is met by heat treatment rather than fumigation, one process covers both the export rules and your need to keep chemicals away from the product.
Are your pharmaceutical pallets new or recycled?
New, every time. CMTP doesn’t supply recycled pallets into pharmaceutical work, because a pallet with an unknown past is exactly the kind of contamination risk an auditor will pick up. You know where the timber came from, how it was treated and when the pallet was made.
Can you provide certificates and documentation for our supplier approval?
Yes. We can supply copies of our HACCP International, ISO 9001 (Colac and Dandenong) and ISPM 15 certifications to support your supplier approval process. If your QA team needs anything else on file, let us know what it is and we’ll sort it out.
Will your pallets suit our racking and automated warehouse?
Yes. Automated storage and pallet racking don’t tolerate a pallet that’s a few millimetres out. The team builds to your exact spec, whether that’s Australian standard (1165 x 1165 mm), Euro or US, and holds that spec batch after batch, so pallets run through your system without jamming.
How do you protect sensitive pharmaceutical equipment in transit?
We design the crate around the equipment, with internal bracing and cushioning to stop it moving and absorb shock on the road. Moisture barriers and VCI (vapour corrosion inhibitor) packaging protect metal parts and electronics from condensation, which matters most on long trips or when equipment is stored before installation.
Can you deliver on a schedule and hold stock for us?
Yes. We can set up scheduled deliveries matched to your production, or make your pallets in bulk, hold them at your nearest CMTP site and release them when you call them off. You keep warehouse space for product, not packaging, and never run short.
Talk to Us Today
Your supply chain is controlled. Your pallets should be too.